

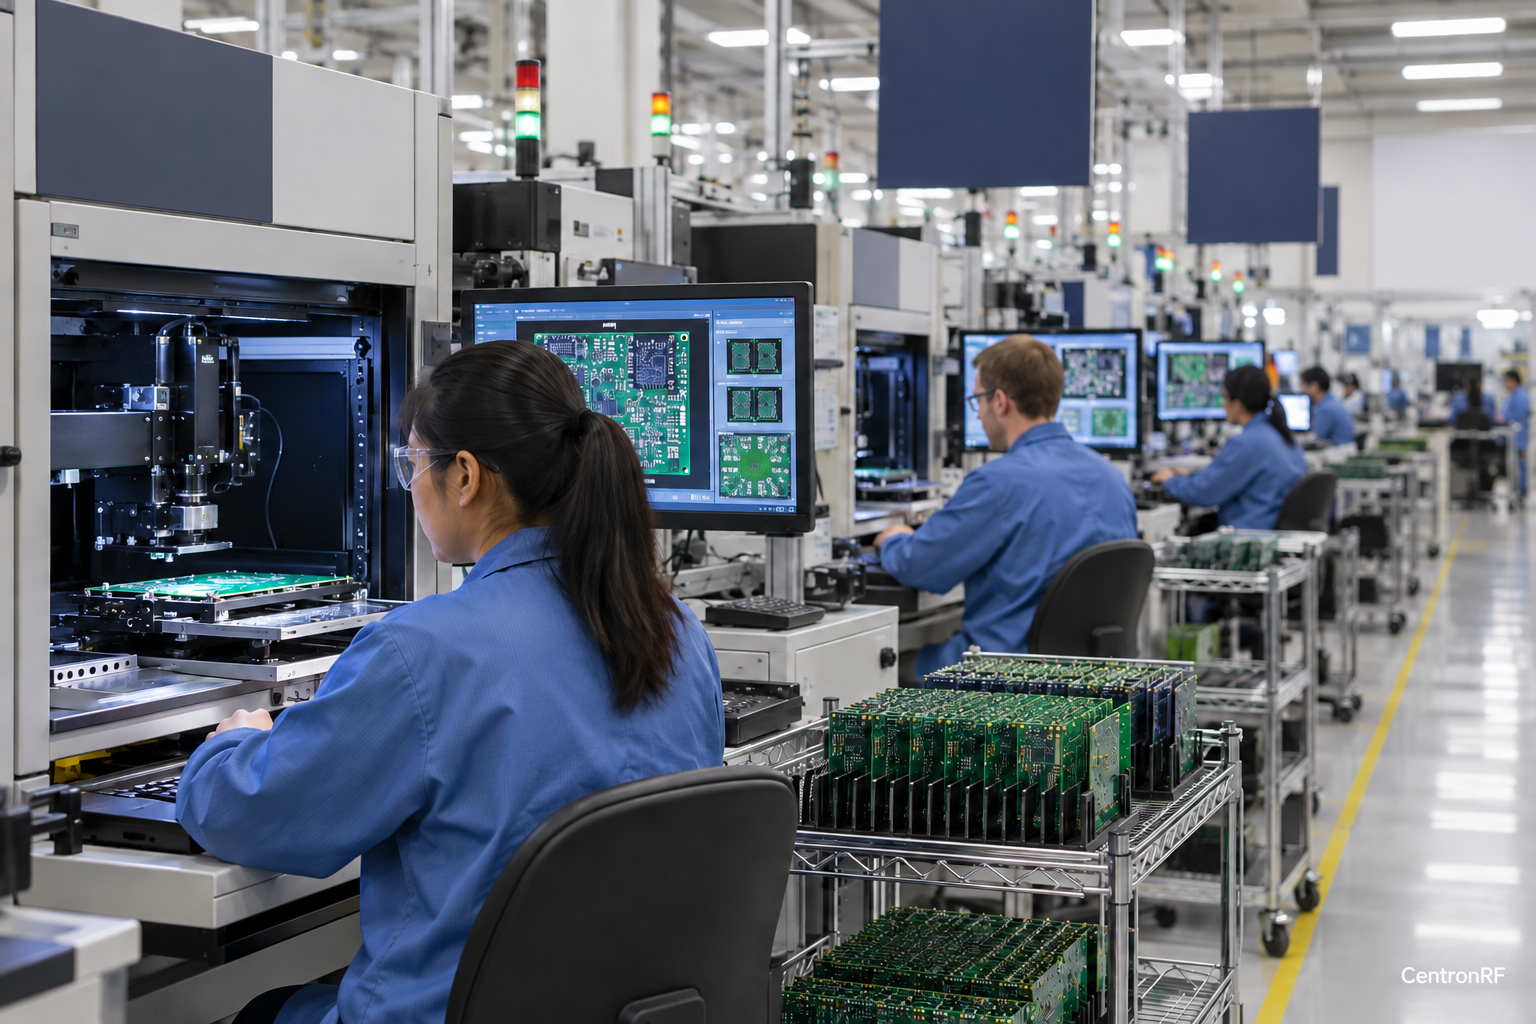
A station handover should leave operators and maintenance teams with a defined configuration, test procedure and response to abnormal results.
Why this matters in the industry
Manufacturers need production readiness that extends beyond an engineering demonstration on a few working devices.
The technical reasoning
A station handover transfers both operating instructions and the evidence needed to recognize abnormal behavior. The receiving team should know the reference plane, correction version, baseline limits and response to failed verification. Demonstrating a known reference run is more informative than assuming the written setup is complete.
Using production data to separate product and station behavior
Manufacturing measurements contain variation from products and from the test process. Stable station offsets, contact wear, reference-device drift and inconsistent retest rules can alter apparent yield. A specification limit defines a product requirement; a process-control limit describes observed process behavior and serves a different purpose. Replacing one with the other can hide defects or create unnecessary rejection, so the data model must distinguish product, station and attempt identity.
How to structure the investigation
Include the fixture drawing, released software, correction files and reference checks. Define connector care, warm-up and fault escalation. Demonstrate the approved workflow with representative units and record open issues before handover.
Preserve first-attempt records and classify confirmed station interruptions separately from completed DUT failures. Trend results by station, product revision, channel and relevant operating state. Use repeated reference checks and controlled cross-station comparisons to investigate shifts. Release corrections or test-limit changes through a documented review, and evaluate whether earlier results were affected when a station fault is discovered.
Worked example or engineering scenario
A handover reference run detects that the new operator selected the wrong fixture profile. Capturing the result and configuration confirms that the transferred method was implemented correctly.
Evidence to collect
| Record | Purpose |
|---|---|
| Released configuration | Defines the tested state and scope of the comparison. |
| Operator procedure | Makes the stimulus or route condition reproducible. |
| Reference check | Supports interpretation of variation and possible confounding effects. |
| Fault escalation | Connects the observation with the stated engineering decision. |
Trade-offs and common interpretation errors
Passing a retest does not erase an intermittent failure, and improved yield does not automatically show improved radio performance. A golden device can itself change. Interpret station trends alongside reference stability and measurement uncertainty, retaining enough detail to distinguish a real process improvement from a changed test decision.
What the result can support
Finish handover with a verified baseline and clear responsibility for configuration changes and fault escalation.
Handover evidence must reflect the actual product variants approved for that station.
Further technical reading
Related industry knowledge
- What Is an RF Production Test Fixture?
- RF Cable Wear: When Should a Production Fixture Cable Be Replaced?
Numerical scenarios are illustrative assumptions, not reported measurements of a supplied product or installation.