

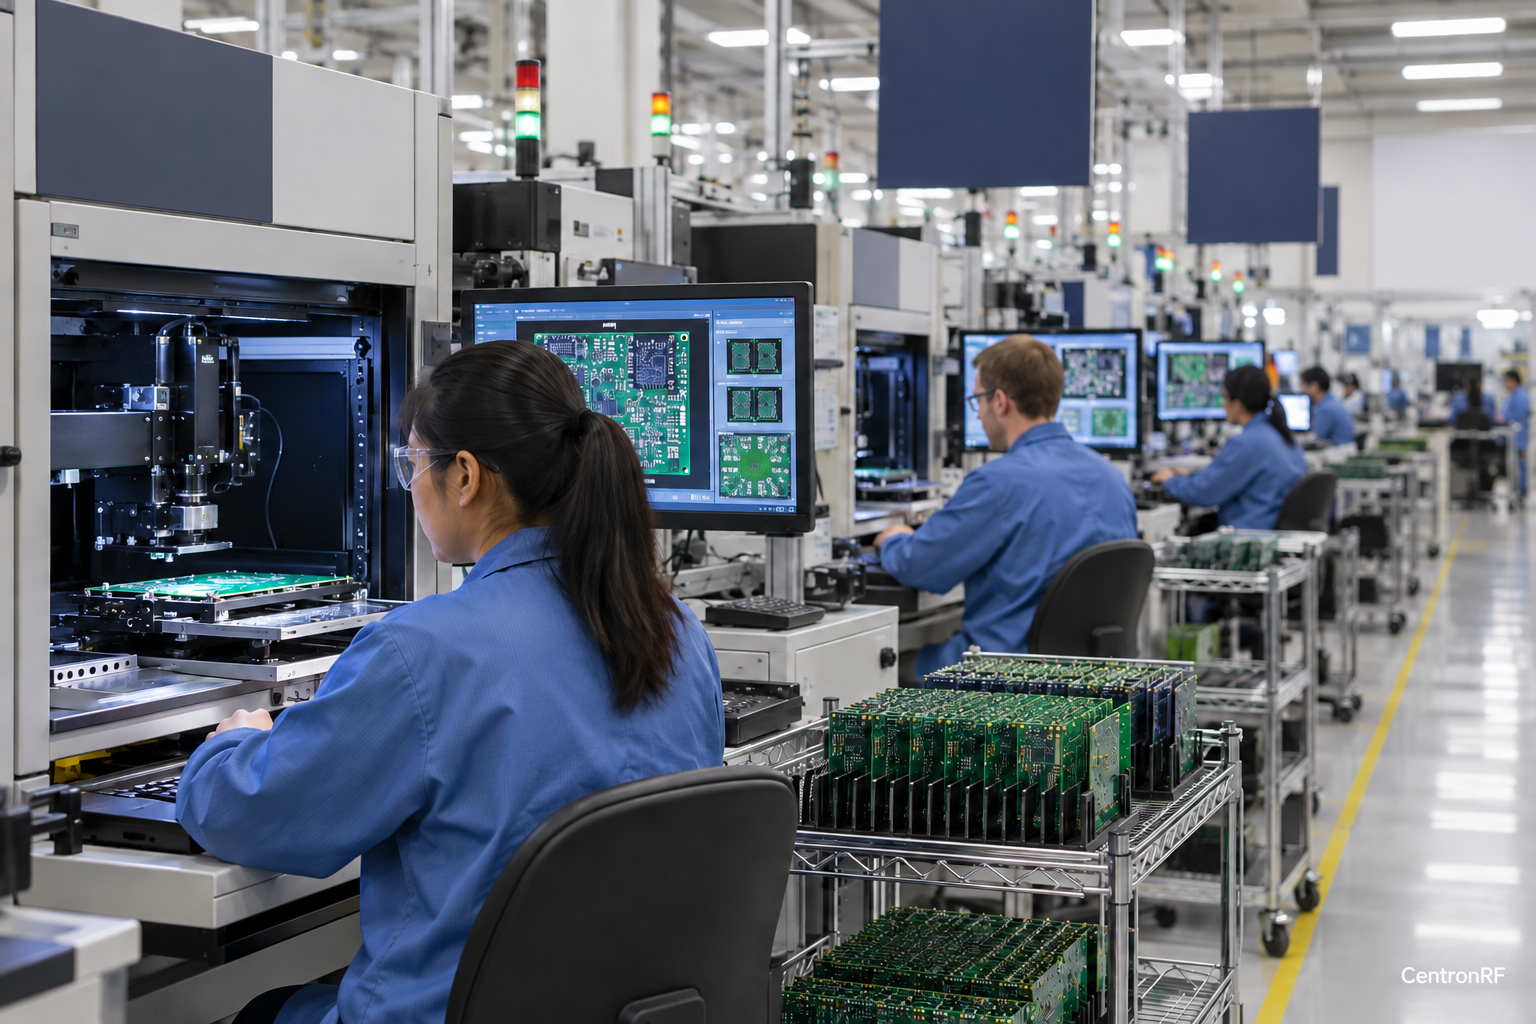
An RF production fixture connects a device under test to repeatable measurement paths while supporting the required electrical and mechanical interfaces.
Why this matters in the industry
Manufacturers need stable connections across many units so fixture variation does not masquerade as a product defect.
The technical reasoning
A production fixture defines the repeatable mechanical and electrical boundary between an assembly and a test station. Its job is to make measurements comparable over many units, operators and cycles. Contact wear, routing variation and software corrections can introduce station-specific bias that looks like manufacturing variation.
Using production data to separate product and station behavior
Manufacturing measurements contain variation from products and from the test process. Stable station offsets, contact wear, reference-device drift and inconsistent retest rules can alter apparent yield. A specification limit defines a product requirement; a process-control limit describes observed process behavior and serves a different purpose. Replacing one with the other can hide defects or create unnecessary rejection, so the data model must distinguish product, station and attempt identity.
How to structure the investigation
Draw every RF route from the instrument to the DUT. Identify calibration planes, replaceable cables and contact interfaces. Measure fixture loss and repeatability before setting acceptance limits, then repeat checks after maintenance.
Preserve first-attempt records and classify confirmed station interruptions separately from completed DUT failures. Trend results by station, product revision, channel and relevant operating state. Use repeated reference checks and controlled cross-station comparisons to investigate shifts. Release corrections or test-limit changes through a documented review, and evaluate whether earlier results were affected when a station fault is discovered.
Worked example or engineering scenario
If every unit tested after a fixture change reads 0.7 dB lower while an independent reference remains stable, investigate the station before attributing the shift to a production process.
Evidence to collect
| Record | Purpose |
|---|---|
| DUT interface | Defines the tested state and scope of the comparison. |
| Fixture revision | Makes the stimulus or route condition reproducible. |
| Route loss | Supports interpretation of variation and possible confounding effects. |
| Connection repeatability | Connects the observation with the stated engineering decision. |
Trade-offs and common interpretation errors
Passing a retest does not erase an intermittent failure, and improved yield does not automatically show improved radio performance. A golden device can itself change. Interpret station trends alongside reference stability and measurement uncertainty, retaining enough detail to distinguish a real process improvement from a changed test decision.
What the result can support
Evaluate fixture repeatability and stability against the measurement differences that drive the production decision.
A fixture description does not establish the accuracy of the complete station.
Further technical reading
Related industry knowledge
Numerical scenarios are illustrative assumptions, not reported measurements of a supplied product or installation.